

Gear pumps are among the most reliable and widely deployed positive displacement pumps in industrial and mobile hydraulic systems worldwide. Their simple design, predictable output, and ability to handle a broad range of fluids make them indispensable across dozens of industries.
This guide covers the gear pump working principle, compares internal and external gear pumps, presents real-world performance data, and provides a practical framework for selecting, sizing, and maintaining these critical components.
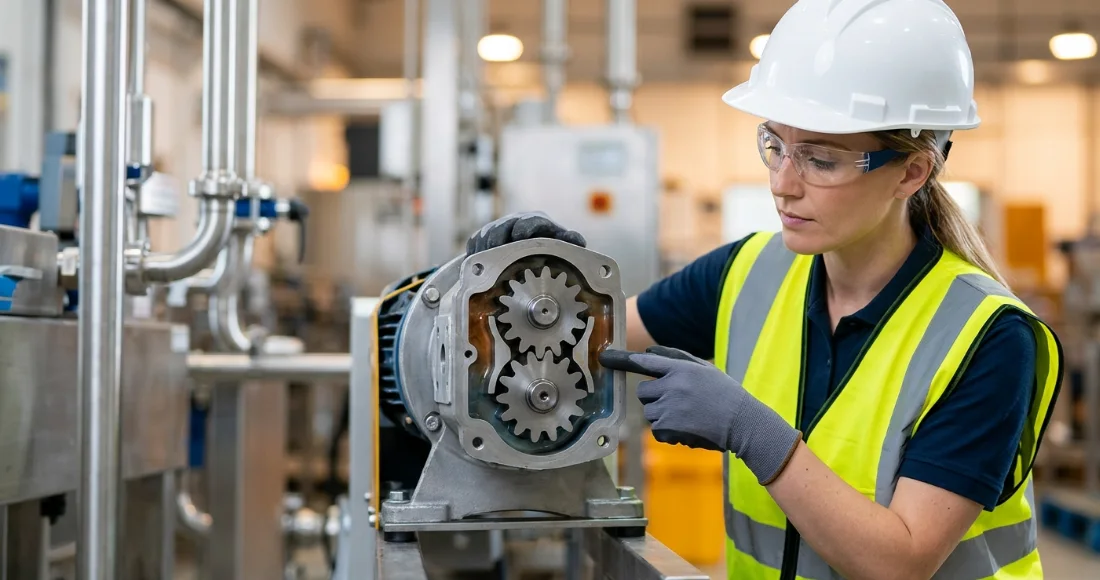
What Is a Gear Pump and How Does It Work
Gear Pump Working Principle Explained
A gear pump operates on the positive displacement pump principle. Two meshing gears rotate inside a tightly fitted casing, trapping fluid in the spaces between the gear teeth and the housing wall.
As the gears rotate, fluid is carried from the inlet (suction) side to the outlet (discharge) side. The meshing point of the gears prevents backflow, creating a continuous, near-pulseless flow proportional to rotational speed.
This mechanism delivers a fixed volume of fluid per revolution, making gear pumps highly predictable. Unlike centrifugal pumps, their output is largely independent of discharge pressure, which is why they excel in hydraulic power systems and metering applications.
Key Components of a Gear Pump
Gears: The heart of the pump. Precision-machined from hardened steel, cast iron, or specialty alloys, the gears create the displacement chambers that move fluid. Tooth profile and surface finish directly impact gear pump flow rate efficiency.
Casing (Housing): The close-tolerance enclosure that contains the gears. Minimal clearance between gear tips and the casing wall reduces internal leakage, also called slip, which preserves volumetric efficiency.
Bearings: Support the gear shafts and maintain precise alignment under load. Journal bearings or needle roller bearings are common, depending on pressure rating and speed requirements.
Seals: Prevent external leakage where the drive shaft exits the housing. Lip seals handle low-pressure applications, while mechanical seals serve high-pressure or hazardous-fluid duties.
Drive Shaft: Connects the pump to the prime mover (electric motor, engine PTO, or hydraulic motor). Proper shaft alignment is critical to bearing life and overall pump longevity.
Types of Gear Pumps — Internal and External Gear Pumps
The two primary configurations of gear pumps differ significantly in construction, performance envelope, and ideal application. External gear pumps use two identical spur or helical gears meshing side by side. Internal gear pumps place a smaller gear (idler) inside a larger ring gear, often separated by a crescent-shaped divider.
External designs deliver higher pressures and suit compact hydraulic circuits. Internal designs handle higher viscosities with lower shear and quieter operation, making them preferred for food processing and polymer transfer.
| Feature | External Gear Pump | Internal Gear Pump |
|---|---|---|
| Flow Range | 1–250 GPM | 1–600 GPM |
| Max Pressure | Up to 3,500 PSI | Up to 1,500 PSI |
| Viscosity Handling | Low to medium | Low to very high |
| Noise Level | Moderate–High | Low |
| Typical Applications | Hydraulics, fuel transfer | Food processing, polymers |
| Cost | Lower | Higher |
Gear Pump Performance Metrics and Efficiency Data
Volumetric and Mechanical Efficiency Benchmarks
Volumetric efficiency measures how much of the theoretical displaced volume actually reaches the outlet. New, properly sized gear pumps typically achieve 85–95% volumetric efficiency, with premium units exceeding 93% under optimal conditions.
Mechanical efficiency accounts for friction losses in bearings, seals, and gear mesh. Combined (overall) efficiency for a well-maintained gear pump generally falls between 80% and 90%.
Efficiency degrades over time due to gear face wear increasing internal clearances, viscosity drops from fluid heating, and seal deterioration allowing internal leakage. Monitoring pressure output at constant speed is the simplest way to track efficiency decline in the field.
Flow Rate Calculations and Real-World Output Data
Theoretical flow rate is calculated as: Displacement (cc/rev) × Speed (RPM) ÷ 1,000 = Flow (LPM). Actual output is always lower due to internal slip. The table below shows real-world performance from popular hydraulic gear pump models.
| Pump Model (Example) | Displacement (cc/rev) | Speed (RPM) | Theoretical Flow (LPM) | Actual Flow (LPM) | Volumetric Efficiency |
|---|---|---|---|---|---|
| Bosch Rexroth AZPF-10 | 8 | 1,500 | 12.0 | 11.1 | 92.5% |
| Parker PGP 505 | 16 | 1,800 | 28.8 | 26.2 | 91.0% |
| Marzocchi GHP2A | 11 | 2,000 | 22.0 | 20.5 | 93.2% |
These figures represent mid-life performance at standard operating temperatures (40–60°C) with ISO VG 46 hydraulic oil. New pumps may test slightly higher; worn units will fall below these benchmarks.
Factors Affecting Gear Pump Flow Rate Efficiency
Fluid Viscosity: Too low and internal leakage increases, reducing volumetric efficiency. Too high and the pump struggles to fill on the suction side, causing cavitation. Most gear pumps perform best between 16–100 cSt at operating temperature.
Operating Temperature: Higher temperatures thin the fluid, increasing slip. Every 10°C rise above optimal can reduce volumetric efficiency by 1–3% depending on clearance design.
Gear Clearance Tolerances: Tighter clearances yield higher efficiency but demand cleaner fluid and more precise manufacturing. Typical gear-to-housing clearances range from 0.02–0.05 mm in quality pumps.
Rotational Speed: Running above rated speed causes incomplete filling (cavitation) and accelerated wear. Running too slowly reduces output without proportional efficiency gains due to fixed leakage paths.
Hydraulic Gear Pump Applications Across Industries
Mobile Hydraulics and Construction Equipment
Gear pumps dominate mobile hydraulic systems due to their compact size, ruggedness, and tolerance of contamination compared to piston or vane alternatives. Parker Hannifin industry data indicates that gear pumps power over 60% of mobile hydraulic circuits globally.
Excavators, wheel loaders, backhoes, and agricultural tractors rely on external gear pumps to drive steering, implement lift, and auxiliary circuits. A typical mid-size excavator may use two or three gear pumps in a tandem or triple configuration to supply independent circuits simultaneously.
Their ability to operate reliably in harsh environments with temperature swings from -20°C to +80°C and exposure to dust and vibration makes them the default choice for off-highway equipment manufacturers like Caterpillar, John Deere, and Komatsu.
Industrial and Manufacturing Systems
In factory settings, gear pumps serve lubrication systems for machine tools, presses, and rolling mills. They deliver precise, consistent oil volumes to bearings, slideways, and gearboxes regardless of back-pressure variations.
Chemical metering applications use gear pumps to dose additives, catalysts, and colorants with repeatable accuracy. Paint spraying systems rely on their steady output to maintain uniform coating thickness.
Die casting machines use hydraulic gear pumps to actuate clamping and injection cylinders where moderate pressures (1,500–2,500 PSI) and reliable duty cycles are required without the cost of piston pump systems.
Automotive and Fuel Systems
Nearly every internal combustion engine uses a gear pump as its oil pump. These internal crescent-type or gerotor pumps circulate lubricating oil through the engine block at pressures of 40–80 PSI, driven directly off the crankshaft or camshaft.
Automatic transmissions employ gear pumps to pressurize transmission fluid for clutch actuation and torque converter charging. Diesel fuel transfer systems use external gear pumps to move fuel from tanks to injection systems at controlled flow rates.
The automotive sector alone accounts for billions of gear pump units in service worldwide, making it the highest-volume application segment even though individual pump sizes are small.
Food, Pharmaceutical, and Chemical Processing
Internal gear pumps excel in processing shear-sensitive and high-viscosity fluids. Chocolate, peanut butter, adhesives, resins, and polymers with viscosities up to 1,000,000 cP are routinely handled by internal gear designs with heated jackets and large clearances.
Sanitary versions built from 316L stainless steel with CIP (clean-in-place) capability meet FDA and 3-A standards for food and pharmaceutical production. Their gentle pumping action preserves product integrity without breaking emulsions or degrading sensitive compounds.
Chemical plants use gear pumps for transferring isocyanates, epoxies, solvents, and other process fluids where precise metering and chemical resistance are essential. Material selection (stainless steel, Hastelloy, or carbon/ceramic internals) is matched to the specific fluid chemistry.
Selecting the Right Gear Pump — Decision Framework
Matching Pump Type to Application Requirements
Choosing between internal and external gear pumps starts with four primary criteria: required operating pressure, fluid viscosity range, flow demand, and chemical compatibility. Secondary factors include noise limits, space constraints, and budget.
For hydraulic power units operating above 2,000 PSI, external gear pumps are almost always the correct choice. For process applications handling thick or shear-sensitive fluids below 1,000 PSI, internal gear pumps deliver superior results.
When the application falls in an overlap zone (moderate pressure, moderate viscosity), consider lifecycle cost. External gear pumps cost less upfront but may require more frequent replacement in viscous-fluid service. Internal gear pumps cost more initially but often deliver lower total cost of ownership in demanding process applications.
Gear Pump Selection Comparison Table
| Selection Criteria | Best Choice | Reason |
|---|---|---|
| High pressure (>2,500 PSI) | External gear pump | Tighter tolerances, rigid design |
| High viscosity (>10,000 cP) | Internal gear pump | Gentle handling, low shear |
| Compact mobile hydraulics | External gear pump | Smaller footprint, lighter weight |
| Quiet operation required | Internal gear pump | Fewer gear contacts, smoother flow |
| Abrasive fluids | Neither (consider alternatives) | Gear wear accelerates rapidly |
For abrasive fluids containing solid particles, progressive cavity pumps or peristaltic pumps are typically better suited. Gear pumps rely on tight clearances that abrasive media destroy quickly, leading to rapid efficiency loss and premature failure.
Common Sizing Mistakes and How to Avoid Them
Over-speeding: Running a gear pump above its rated RPM to achieve higher flow causes cavitation, excessive noise, and accelerated wear. Instead, select a larger displacement pump running at moderate speed for the same output with longer life.
Ignoring viscosity-temperature curves: Fluid viscosity changes dramatically with temperature. A pump sized for cold-start viscosity may cavitate; one sized for hot running viscosity may slip excessively at startup. Always evaluate the full operating temperature range.
Undersizing inlet piping: Gear pumps are not self-priming in the same way as some other positive displacement types. Restricted or undersized suction lines create vacuum conditions that cause cavitation, noise, and bearing damage. Inlet velocity should stay below 1.2 m/s for most hydraulic oils.
Neglecting system pressure spikes: Sizing only for steady-state pressure ignores transient spikes from valve closures or load changes. Select a pump rated at least 20% above maximum expected system pressure to maintain seal integrity and bearing life.
Maintenance, Troubleshooting, and Lifespan Optimization
Preventive Maintenance Schedule
Every 500 hours: Check fluid level and condition visually. Inspect for external leaks at shaft seal and port connections. Verify operating temperature stays within specification.
Every 2,000 hours: Perform fluid analysis (particle count, viscosity, water content, oxidation level). Replace filters. Check coupling alignment and mounting bolt torque.
Every 5,000 hours: Measure gear wear using backlash or flow-at-pressure testing. Inspect bearings for play. Replace shaft seals proactively if operating in dusty or wet environments. Evaluate whether volumetric efficiency has dropped below 85%, which signals the need for rebuild or replacement.
Diagnosing Common Gear Pump Failures
Cavitation noise (high-pitched whine or rattling): Caused by insufficient fluid reaching the inlet. Check for clogged suction strainers, collapsed inlet hoses, excessive fluid viscosity at cold start, or air leaks in suction plumbing.
Pressure loss at constant speed: Indicates increased internal leakage from worn gear faces, side plates, or housing bore. Measure case drain flow if available; rising case drain confirms internal wear.
Overheating: Excessive internal leakage converts hydraulic energy to heat. Also caused by operating above rated pressure, inadequate reservoir cooling, or fluid viscosity too low for the clearances.
External leakage: Shaft seal failure from misalignment, excessive pressure spikes, or chemical attack on seal material. Port fitting leaks from vibration-loosened connections or damaged O-rings.
Extending Service Life Beyond 10,000 Hours
Filtration: Maintain fluid cleanliness to ISO 18/16/13 or better. Use 10-micron absolute return-line filters as a minimum. Particles larger than the pump's internal clearances cause abrasive wear that compounds over time.
Correct fluid selection: Match fluid viscosity grade to the pump manufacturer's recommendation for the operating temperature range. ISO VG 32–68 covers most hydraulic gear pump applications. Ensure the fluid's additive package is compatible with pump seal materials.
Alignment: Misalignment between the pump shaft and drive motor creates radial loads that bearings are not designed to carry. Use flexible couplings and verify alignment to within 0.05 mm TIR (total indicator runout) at installation and after any maintenance.
Proper startup procedures: Fill the pump casing with fluid before first start. Run at low pressure for several minutes to purge air and allow bearings to develop a hydrodynamic film before applying full load.
Frequently Asked Questions (FAQ)
What is the difference between internal and external gear pumps?
External gear pumps use two identical meshing gears rotating in opposite directions inside a housing. Internal gear pumps use a smaller gear (idler) rotating inside a larger ring gear, often separated by a crescent-shaped partition. External types excel at high-pressure hydraulic applications up to 3,500 PSI. Internal types handle viscous fluids more gently with lower noise and less shear, making them ideal for food processing and polymer transfer.
How do I calculate gear pump flow rate?
Use the formula: Flow (LPM) = Displacement (cc/rev) × Speed (RPM) ÷ 1,000. This gives theoretical output. Multiply by volumetric efficiency (typically 0.85–0.95) to get actual delivered flow. For example, a 10 cc/rev pump at 1,500 RPM with 90% efficiency delivers: 10 × 1,500 ÷ 1,000 × 0.90 = 13.5 LPM actual flow.
What industries use hydraulic gear pumps most?
Construction and agriculture represent the largest market segments, with gear pumps powering the majority of mobile hydraulic circuits in excavators, loaders, and tractors. Manufacturing, automotive, and food processing follow closely. The automotive sector has the highest unit volume due to engine oil pumps and transmission pumps installed in every vehicle produced.
How long does a gear pump last?
With proper maintenance, clean fluid (ISO 18/16/13 cleanliness), correct viscosity, and operation within rated parameters, gear pumps commonly achieve 10,000–20,000 operating hours. Premium pumps in well-maintained systems can exceed 25,000 hours. Harsh conditions, contaminated fluid, or chronic over-pressurization can reduce service life below 5,000 hours.
Can gear pumps handle water or only oil?
Standard gear pumps are engineered for oil-based fluids that provide lubrication to internal surfaces. Specialized versions with stainless steel housings, carbon or ceramic bearings, and compatible seals can handle water and water-glycol fluids. However, the low lubricity of water increases wear rates, and efficiency may be reduced due to the low viscosity increasing internal slip. Always consult the manufacturer for water-service ratings.
Why is my gear pump losing pressure?
The most common cause is increased internal clearance from worn gear faces or side plates, allowing fluid to leak from the high-pressure side back to the low-pressure side. Other causes include damaged shaft seals reducing volumetric output, cavitation from restricted inlet flow starving the pump, or a malfunctioning relief valve diverting flow back to tank. Measure flow at rated speed and compare to the pump's original specification to quantify the efficiency loss and determine whether repair or replacement is needed.



