

Hydraulic motors are the workhorses behind countless industrial and mobile equipment applications. Knowing how to properly inspect and replace their internal components is essential for minimizing downtime and extending service life.
This guide walks you through the complete process of hydraulic motor repair, from pre-inspection safety procedures through post-replacement validation. Whether you're performing routine hydraulic system maintenance or diagnosing an unexpected failure, these procedures will help you work efficiently and accurately.
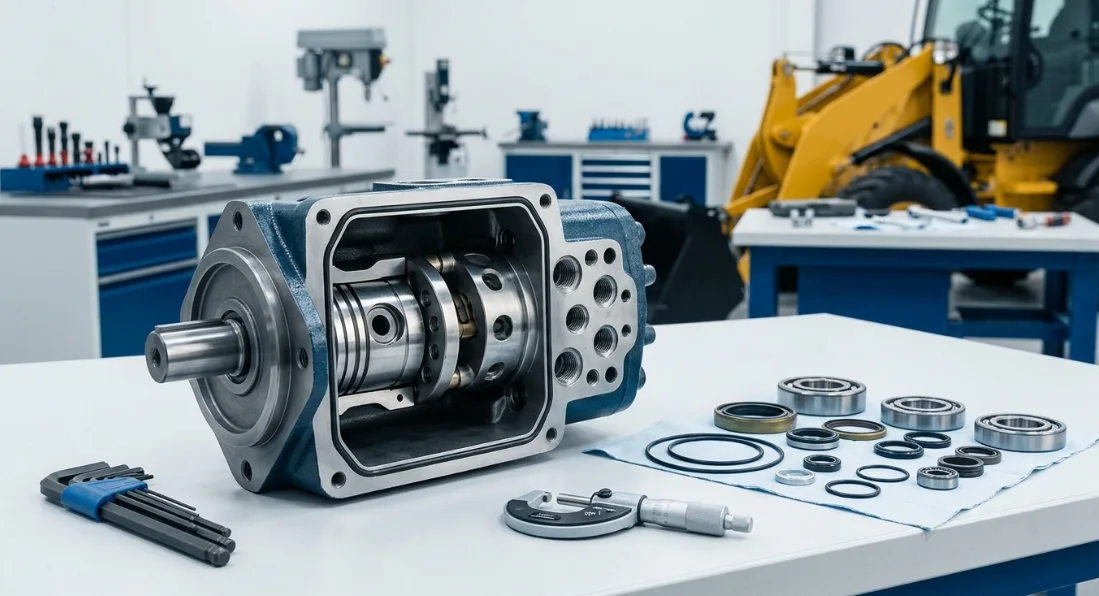
Understanding Hydraulic Motor Systems
Types of Hydraulic Motors
Hydraulic motors convert fluid pressure and flow into rotational mechanical energy. The three primary types each serve distinct roles across industrial and mobile equipment.
Gear motors are the simplest and most cost-effective option. They use meshing gears to produce rotation and are commonly found in conveyors, augers, and low-to-medium pressure applications where precise speed control is less critical.
Vane motors offer smoother operation and better volumetric efficiency than gear types. They're widely used in machine tools, plastics machinery, and applications requiring consistent torque at moderate pressures.
Piston motors deliver the highest pressure ratings and efficiency. Available in axial and radial configurations, they power heavy-duty equipment such as excavators, winches, and high-performance industrial drives where maximum power density is required.
Key Components Subject to Wear
Every hydraulic motor contains components that degrade over time due to pressure cycling, fluid contamination, and mechanical stress. Understanding what fails and why is the foundation of effective hydraulic component wear diagnosis.
| Component | Function | Common Failure Mode | Inspection Frequency |
|---|---|---|---|
| Shaft seals | Prevent fluid leakage | Hardening, cracking | Every 500 hours |
| Bearings | Support rotating shaft | Pitting, spalling | Every 1,000 hours |
| Gears/Pistons | Convert pressure to rotation | Scoring, erosion | Every 2,000 hours |
| End caps | Contain internal pressure | Warping, corrosion | Every 2,000 hours |
| O-rings | Seal static joints | Compression set, extrusion | Every 500 hours |
| Valve plates | Direct fluid flow | Scoring, cavitation damage | Every 2,000 hours |
These intervals represent general guidelines. Harsh operating environments, high duty cycles, or poor fluid conditions may require more frequent inspection.
Pre-Inspection Preparation
Safety Procedures and System Depressurization
Hydraulic systems store tremendous energy even when the machine is shut down. Proper depressurization is non-negotiable before any inspection or disassembly work begins.
Follow these steps to safely prepare the system:
- Shut down the prime mover (electric motor or engine) and verify it cannot restart.
- Apply lockout/tagout (LOTO) to all energy sources, including electrical, pneumatic, and mechanical.
- Cycle all control valves to relieve trapped pressure in actuator lines.
- Verify zero pressure on system gauges at the motor inlet and outlet ports.
- Allow the system to cool if fluid temperature exceeds 120°F to prevent burns.
- Place absorbent materials beneath the motor to catch residual fluid during disconnection.
Never assume a system is depressurized based on gauge readings alone. Blocked lines and check valves can trap pressure in isolated sections of the circuit.
Tools and Equipment Required
Having the correct tools organized before disassembly prevents contamination from repeated trips to the toolbox and ensures accurate measurements during hydraulic component wear diagnosis.
| Tool Category | Specific Items | Purpose |
|---|---|---|
| Measurement | Micrometers, dial indicators, feeler gauges | Dimensional verification |
| Disassembly | Torque wrenches, pullers, seal picks | Safe component removal |
| Diagnostic | Pressure gauges, flow meters, thermometers | Performance baseline |
| Cleanliness | Lint-free cloths, solvent, clean containers | Contamination prevention |
| Documentation | Camera, logbook, manufacturer specs | Record keeping |
Always calibrate measurement tools before use. An out-of-calibration micrometer can lead to accepting worn components that should be replaced.
Evaluating Hydraulic Fluid Contamination
Fluid condition tells you more about internal motor health than almost any external inspection. Hydraulic fluid contamination is the leading cause of premature component failure in hydraulic systems.
Take fluid samples from the motor case drain port and the system return line before disassembly. Use clean sample bottles and follow proper sampling procedures to avoid introducing external contaminants into the analysis.
Key fluid analysis indicators to evaluate:
- ISO cleanliness code: Compare current particle counts against the OEM-recommended cleanliness level for your motor type.
- Water content: Levels above 0.1% accelerate seal degradation and promote corrosion on internal surfaces.
- Metallic particle analysis: Iron indicates gear or bearing wear. Bronze suggests bushing or valve plate degradation. Aluminum points to housing or piston shoe wear.
- Viscosity deviation: Fluid that has thinned or thickened beyond specification cannot maintain proper lubrication films.
Document all fluid analysis results and correlate them with the physical wear patterns found during disassembly. This data builds a maintenance history that improves future hydraulic system maintenance decisions.
Step-by-Step Inspection Process
External Visual Inspection
Before removing a single bolt, conduct a thorough external assessment. Many failure modes leave visible evidence on the outside of the motor housing.
Check for these external indicators:
- Fluid leaks: Trace leak paths to their origin. Shaft seal leaks indicate internal pressure issues or seal wear. Port connection leaks suggest O-ring failure or improper torque.
- Housing cracks: Inspect the motor body for stress fractures, particularly around mounting feet and port bosses.
- Mounting bolt condition: Loose or broken mounting bolts cause misalignment that accelerates bearing and seal wear.
- Shaft condition: Check the exposed shaft for scoring, corrosion, or fretting where couplings attach.
- Unusual noise or vibration: If the motor is still operational, note any grinding, knocking, or whining sounds that indicate internal damage.
Photograph all findings before proceeding. These images become valuable reference points when ordering replacement parts and documenting the repair.
Disassembly Sequence
Proper disassembly preserves critical alignment relationships and prevents additional damage to reusable components. Always follow the manufacturer's recommended sequence when available.
General disassembly guidelines:
- Mark all components with orientation indicators before removal. Use a paint pen or scribe to mark mating surfaces, port positions, and rotational alignment.
- Remove port fittings and plug all openings immediately to prevent contamination entry.
- Remove end cap bolts in a star pattern, loosening gradually to prevent warping.
- Separate the end cap carefully. Internal springs or check valves may be under light preload.
- Remove the rotating group (gears, pistons, or vanes) as an assembly when possible.
- Extract bearings and seals last, using appropriate pullers to avoid bore damage.
Place all components on a clean, lint-free surface in the order they were removed. This simplifies reassembly and ensures nothing is overlooked during inspection.
Internal Component Wear Diagnosis
Accurate measurement is the core of hydraulic component wear diagnosis. Each critical dimension must be compared against OEM specifications to determine whether a component is serviceable or requires replacement.
| Wear Indicator | Measurement Method | Acceptable Tolerance | Action if Exceeded |
|---|---|---|---|
| Shaft journal wear | Micrometer measurement | ±0.001" from spec | Replace shaft |
| Gear tooth backlash | Feeler gauge | 0.002"–0.005" | Replace gear set |
| Bore scoring | Visual + profilometer | Ra < 16 μin | Hone or replace housing |
| Seal groove damage | Visual inspection | No nicks or burrs | Machine or replace |
| Piston clearance | Bore gauge | Per OEM spec | Replace piston/barrel |
| Valve plate flatness | Surface plate + indicator | < 0.0005" deviation | Lap or replace |
Take multiple measurements at different points on each component. A shaft may measure within tolerance at one location but show localized wear at the seal contact area. Record all readings for comparison during future inspections.
Always replace components as matched sets when specified by the manufacturer. Installing a new gear against a worn mating gear accelerates wear on both parts and reduces motor efficiency.
Hydraulic Pump Troubleshooting Integration
Motor damage doesn't always originate at the motor. Upstream hydraulic pump issues frequently cause downstream motor failures that will recur if the root cause isn't addressed.
Perform these cross-system checks during any motor inspection:
- Pressure spikes: A failing pump relief valve or sticking directional valve can subject the motor to pressures far exceeding its rating, causing seal blowout and bearing damage.
- Cavitation damage: Pump inlet restrictions create vapor bubbles that collapse violently inside the motor, eroding valve plates and piston faces.
- Flow irregularities: A worn pump delivers pulsating flow that causes motor vibration, accelerating bearing fatigue and gear tooth wear.
- Contamination generation: A deteriorating pump introduces metallic particles into the fluid that abrade motor internals.
Hydraulic pump troubleshooting should be a standard part of every motor repair procedure. Replacing motor components without verifying pump health often results in repeat failures within a short operating period.
Component Replacement Procedures
Seal and O-Ring Replacement
Seals are the most frequently replaced components during hydraulic motor repair. Proper installation technique is critical because a damaged seal during installation will leak immediately or fail prematurely.
Follow these seal replacement best practices:
- Remove old seals using brass or plastic picks only. Steel tools can scratch seal grooves and bore surfaces.
- Clean all seal grooves thoroughly, removing any hardened seal material or debris.
- Inspect groove dimensions and surface finish before installing new seals.
- Lubricate new seals with clean hydraulic fluid or the manufacturer's recommended assembly lubricant.
- Use tapered installation sleeves for shaft seals to prevent lip damage during installation over keyways or splines.
- Ensure O-rings are not twisted in their grooves. A twisted O-ring will develop a spiral leak path under pressure.
Always use OEM-specified seal materials. Aftermarket seals may not be compatible with the system fluid or rated for the operating temperature and pressure range.
Bearing and Shaft Replacement
Bearing replacement requires precision to ensure proper fit, alignment, and preload. Incorrect installation is a leading cause of premature bearing failure in rebuilt hydraulic motors.
Key procedures for bearing and shaft replacement:
- Verify the new bearing's dimensions match OEM specifications. Check bore, outer diameter, and width.
- Heat the bearing housing to 200–250°F for interference-fit outer races, or cool the bearing for inner race installation.
- Press bearings using a properly sized driver that contacts only the press-fit race. Never apply force through the rolling elements.
- Check shaft fit with the new bearing. The shaft journal should show no wear marks, scoring, or diameter reduction.
- Verify end play with a dial indicator after installation. Excessive end play causes axial shuttling that damages thrust surfaces.
- Set bearing preload per manufacturer specifications using shims or lock nuts as applicable.
If the shaft shows wear at the bearing journal, replace it rather than attempting to build up material. Shaft repairs rarely achieve the surface finish and dimensional accuracy required for reliable bearing operation.
Gear and Piston Assembly Replacement
Rotating group replacement is the most involved procedure in hydraulic motor repair. These components must be matched, timed, and dimensionally verified before reassembly.
Critical steps for gear and piston replacement:
- Matched sets: Always replace gears as a pair. Pistons and barrels are typically matched during manufacturing and must be replaced together.
- Timing marks: Verify that timing marks on new components align with the motor's design intent. Incorrect timing causes efficiency loss and potential mechanical interference.
- Dimensional verification: Measure all critical clearances with new components installed. Confirm piston-to-bore clearance, gear-to-housing clearance, and end clearance meet specifications.
- Surface condition: Inspect all mating surfaces for shipping damage or protective coating residue that must be removed before assembly.
- Lubrication: Pre-lubricate all rotating and sliding surfaces with clean hydraulic fluid during assembly to prevent dry-start damage.
For piston motors, verify that the swashplate or cam ring surface is within specification. A worn swashplate will destroy new pistons and shoes rapidly.
Reassembly Torque Specifications
Proper torque application ensures even clamping force, prevents distortion, and maintains seal integrity. Under-torqued fasteners leak. Over-torqued fasteners warp housings and strip threads.
| Fastener Location | Typical Torque Range | Torque Pattern | Lubricant Required |
|---|---|---|---|
| End cap bolts | 35–65 ft-lbs | Star pattern | Thread sealant |
| Mounting bolts | 50–90 ft-lbs | Alternating | Anti-seize |
| Port fittings | 20–40 ft-lbs | Sequential | O-ring lube |
| Shaft coupling | Per OEM spec | Single | Dry or Loctite |
Always torque fasteners in multiple passes, typically 50%, 75%, and then 100% of final value. This progressive approach distributes clamping load evenly and prevents gasket or seal damage from uneven compression.
Use a calibrated torque wrench for every fastener. "Feel" is not an acceptable substitute for measured torque in hydraulic motor assembly.
Post-Replacement Testing and Validation
Break-In Procedure
Newly assembled hydraulic motors require a controlled break-in period to allow mating surfaces to conform and seals to seat properly. Skipping this step is a common cause of early failure after hydraulic motor repair.
Follow this general break-in sequence:
- No-load operation: Run the motor at 50% of rated speed with no external load for 5–10 minutes. Monitor case drain flow and temperature.
- Low-load operation: Apply 25% of rated load at 50% speed for 10 minutes. Listen for unusual sounds and check for leaks.
- Progressive loading: Increase load in 25% increments, running 5–10 minutes at each level while monitoring all parameters.
- Full-load verification: Operate at rated conditions for 15–30 minutes. Confirm stable pressure, temperature, and speed.
If case drain flow increases suddenly or temperature rises abnormally during break-in, stop immediately and investigate. These symptoms indicate internal clearance problems or contamination.
Performance Verification
After break-in, perform quantitative testing to confirm the motor meets its rated performance specifications. Document all results for baseline comparison during future hydraulic system maintenance inspections.
| Test Parameter | Target Value | Test Duration | Failure Criteria |
|---|---|---|---|
| Case drain flow | < 5% of system flow | 10 minutes | Exceeds 8% |
| Operating temperature | Within 20°F of baseline | 30 minutes | Continuous rise |
| Output speed | ±5% of rated RPM | 5 minutes | Fluctuation > 10% |
| System pressure | Stable at set point | 15 minutes | Drift > 50 PSI |
| External leakage | Zero visible leaks | Full test cycle | Any drip |
Case drain flow is the single most telling indicator of internal motor condition. Elevated case drain means fluid is bypassing the rotating group internally, reducing efficiency and generating heat.
Compare all test results against the motor's original commissioning data when available. This comparison reveals whether the repair has fully restored performance or if additional work is needed.
Preventive Hydraulic System Maintenance Schedule
Routine Maintenance Intervals
Consistent preventive maintenance dramatically extends the interval between major hydraulic motor repairs. A structured schedule catches developing problems before they cause catastrophic failure.
| Interval | Task | Benefit |
|---|---|---|
| Daily | Check fluid level, listen for noise | Early detection |
| Weekly | Inspect for external leaks | Prevent contamination |
| Monthly | Check filter indicators, fluid temp | Maintain fluid health |
| Quarterly | Sample and analyze fluid | Detect internal wear |
| Annually | Full hydraulic motor repair inspection | Extend service life |
The most effective maintenance programs combine time-based intervals with condition-based monitoring. Fluid analysis trends and vibration data often reveal problems weeks before they become audible or visible.
Extending Component Life
Beyond scheduled inspections, several operational practices significantly reduce wear rates and extend the time between component replacements.
Filtration upgrades: Install filters rated at least two ISO cleanliness codes better than the motor manufacturer's minimum requirement. High-efficiency filters on the return line and case drain line protect motor internals from abrasive particles.
Fluid selection: Use the fluid type and viscosity grade specified by the motor manufacturer. Premium fluids with anti-wear additives and oxidation inhibitors provide better protection than economy alternatives.
Temperature management: Keep fluid temperature between 100°F and 140°F during operation. Install heat exchangers if the system consistently runs above 150°F. Every 18°F above optimal temperature cuts fluid life in half.
Operational load management: Avoid sustained operation at maximum pressure and speed simultaneously. Reduce shock loading through proper valve acceleration and deceleration settings. Smooth operation reduces peak stresses on bearings, gears, and seals.
These practices work together as a system. Clean fluid at the right temperature and viscosity, flowing through a properly loaded motor, delivers maximum component life and minimum unplanned downtime.
FAQ
How do I know when a hydraulic motor needs component replacement versus a full rebuild?
If wear diagnosis shows two or more major components outside tolerance, or if the motor has exceeded its rated service hours by more than 20%, a full rebuild is typically more cost-effective than individual part replacement. A rebuild ensures all components are restored to specification simultaneously, eliminating the risk of a worn part damaging a newly replaced one. Single-component replacements make sense only when one part has failed prematurely while the rest remain within tolerance.
What causes premature hydraulic motor component failure?
The most common causes are hydraulic fluid contamination from particle or water ingress, operating above rated pressure or speed, inadequate filtration, and improper break-in after previous repairs. Contamination alone accounts for over 70% of hydraulic component failures across the industry. Addressing fluid cleanliness through proper filtration and sealed reservoirs is the single most impactful step for preventing premature wear.
Can I mix component brands when replacing hydraulic motor parts?
It is not recommended. OEM-matched components ensure proper clearances and material compatibility. Mixing brands can void warranties and introduce tolerance stack-up issues that accelerate wear. Even if individual dimensions appear correct, differences in material hardness, surface finish, and heat treatment between manufacturers can cause uneven wear patterns and reduced motor efficiency.
How does hydraulic pump troubleshooting relate to motor inspection?
Pump issues such as cavitation, pressure spikes, or flow irregularities directly damage motor internals. Always verify pump health before concluding that motor components failed independently. A worn pump generating contamination or pressure instability will destroy a newly rebuilt motor in a fraction of its expected service life. Comprehensive hydraulic pump troubleshooting should be standard practice during every motor repair event.
What fluid analysis results indicate motor component wear?
Elevated iron and bronze particle counts, increasing ISO cleanliness codes, and the presence of metallic flakes in filter elements all point to internal hydraulic component wear that warrants immediate inspection. Trending these values over time is more informative than any single sample. A sudden spike in wear metals, even if absolute values seem moderate, indicates an accelerating failure that requires prompt attention.
How long does a typical hydraulic motor component replacement take?
Simple seal replacements take 2–4 hours. Full bearing and gear replacements require 6–10 hours depending on motor size, accessibility, and whether the motor is removed from the machine. Add time for fluid sampling



