A hydraulic pump operating at 82% volumetric efficiency doesn't announce its impending failure with alarms or warning lights. It bleeds performance silently, pushing system temperatures higher, slowing cycle times by fractions of a second, and quietly costing thousands in wasted energy before catastrophic failure forces an unplanned shutdown.
This guide covers the complete methodology for testing hydraulic pumps, from baseline flow measurement through advanced diagnostics. Whether you're validating a suspect unit on the bench or performing in-circuit hydraulic system diagnostics, the procedures here follow ISO 4409 standards and reflect current best practices used in industrial maintenance programs.
Why Hydraulic Pump Testing Is Critical for System Reliability
Undetected pump degradation follows a predictable curve. Internal clearances increase gradually, allowing more fluid to bypass from high-pressure to low-pressure zones. The system compensates by running longer cycles, generating more heat, and accelerating wear on every downstream component.
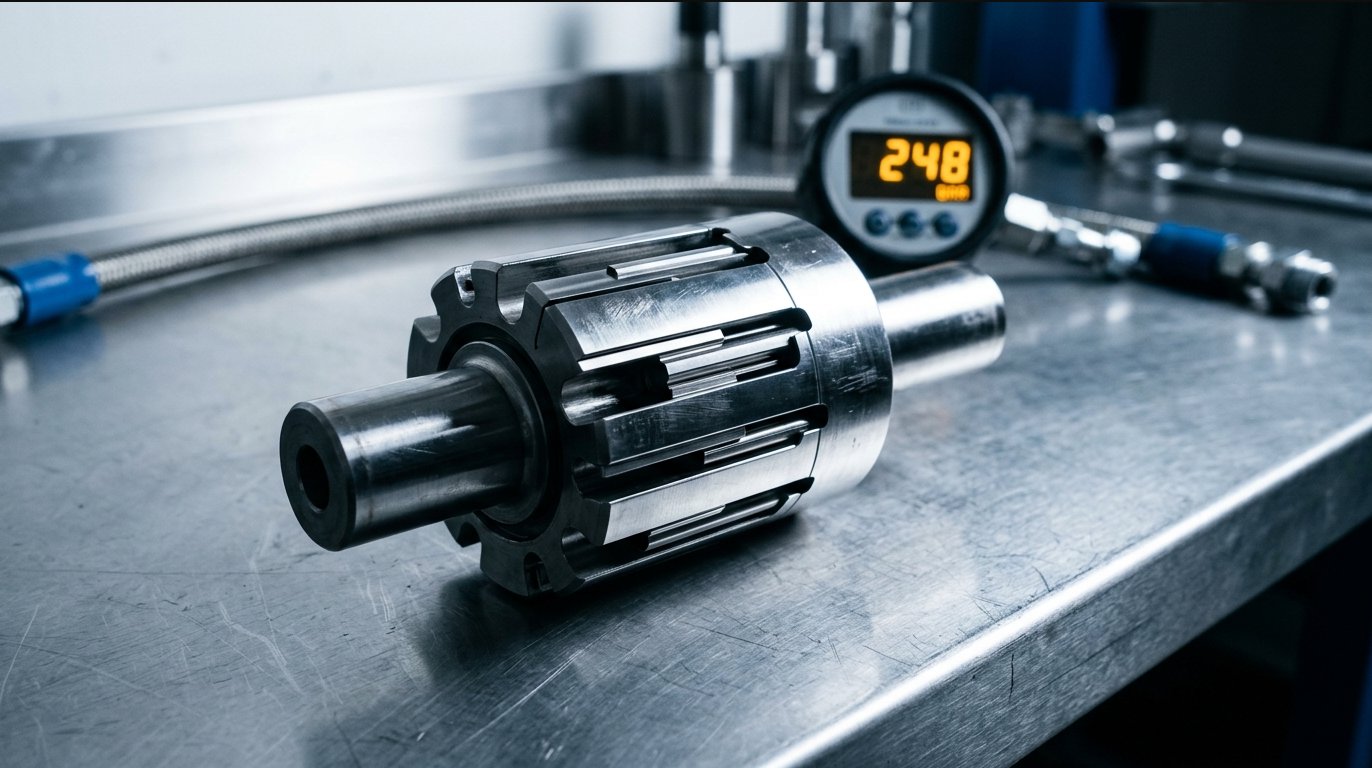
Reactive maintenance after a pump failure typically costs 4–8 times more than a planned replacement when factoring in emergency parts procurement, unplanned labor, production losses, and collateral damage to valves, cylinders, and contaminated fluid. Preventive testing identifies efficiency losses at the point where scheduled intervention remains economical.
Common Symptoms That Indicate a Pump Requires Testing
- Excessive noise: Cavitation (high-pitched whine) or aeration (erratic knocking) both indicate abnormal operating conditions that accelerate wear
- Slow actuator response: Cylinder extension or motor speed declining from established benchmarks suggests reduced flow delivery
- Elevated operating temperatures: Internal leakage converts hydraulic energy to heat, often raising fluid temperature 10–20°C above normal baselines
- Inconsistent pressure readings: Fluctuating gauge needles under steady-state load point toward worn internal components or control instability
Safety Precautions Before Testing
Hydraulic systems store energy in multiple forms. Before connecting any test equipment, complete these mandatory safety steps:
- Lockout/tagout: Isolate all energy sources including electrical, pneumatic pilot supplies, and gravity-loaded actuators per OSHA 29 CFR 1910.147
- Pressure bleed-down: Cycle directional valves to relieve trapped pressure in all circuit branches. Verify with gauges before breaking connections
- PPE requirements: Safety glasses with side shields, hydraulic-rated gloves, and face shield when working near pressurized fittings. Injection injuries from pinhole leaks require immediate emergency medical attention
- Fluid temperature: Allow system to reach operating temperature (40–60°C) before testing, but never connect or disconnect fittings on fluid above 50°C without heat-resistant protection
Essential Equipment for Hydraulic Pump Testing
Accurate hydraulic pump pressure testing and flow rate measurement demand properly calibrated instruments matched to the system under test. Using equipment with insufficient range or resolution produces misleading data that can lead to incorrect maintenance decisions.
Core Testing Instruments
| Equipment | Function | Typical Accuracy |
|---|---|---|
| Hydraulic flow meter | Measures actual pump output (GPM/LPM) | ±0.5–2% |
| Pressure gauge (analog/digital) | Reads system and test pressures | ±0.25–1% FS |
| Infrared thermometer / thermocouple | Monitors fluid and case temperature | ±1°C |
| Tachometer | Verifies pump shaft RPM | ±0.05% |
| Load valve (flow control) | Simulates system load for testing | N/A |
| Case drain flow meter | Detects internal leakage | ±0.5% |
All pressure and flow instruments should carry current calibration certificates traceable to national standards. For critical applications, calibration intervals of 6–12 months are standard practice.
Selecting the Correct Flow Meter Type
Gear-type meters offer broad viscosity tolerance and durability, making them the default choice for portable hydraulic test units. They handle contaminated fluid better than precision meters but introduce slightly higher pressure drop.
Turbine meters provide excellent accuracy at higher flow rates and lower viscosities. They're ideal for bench testing with clean, conditioned fluid but are susceptible to damage from particulate contamination.
Ultrasonic (clamp-on) meters require no pipe cutting or fluid contact, making them valuable for in-system flow rate measurement on live circuits. However, accuracy depends heavily on pipe condition, fluid homogeneity, and proper installation technique.
Match meter capacity to pump displacement with adequate margin. A meter operating below 20% or above 80% of its rated range delivers reduced accuracy. For variable displacement pumps, select a meter that covers the full range from standby to maximum flow.
How to Perform a Hydraulic Pump Flow Test (Step-by-Step)
This procedure covers the standard flow and pressure test method applicable to both fixed and variable displacement pumps. It forms the foundation of any hydraulic pump efficiency evaluation.
Step 1 — Establish Baseline Conditions
Before connecting any test equipment, gather and verify these reference parameters:
- Nameplate data: Record pump displacement (cc/rev or in³/rev), rated RPM, maximum continuous pressure, and manufacturer part number
- Fluid condition: Verify viscosity is within the pump manufacturer's specified range. Most hydraulic pumps are rated for 16–36 cSt at operating temperature
- System readiness: Confirm reservoir level is at operating mark, suction strainers and pressure filters are not in bypass, and all circuit valves are in their normal operating positions
Calculate theoretical maximum flow using: Theoretical Flow (LPM) = Displacement (cc/rev) × RPM ÷ 1000. This value becomes your reference denominator for efficiency calculations.
Step 2 — Install Test Equipment
Install the flow meter downstream of the pump outlet and upstream of any directional control valves. This placement measures actual pump delivery without influence from downstream pressure drops or valve leakage.
Position the load valve downstream of the flow meter. This allows you to simulate system resistance while observing flow changes in real time. Connect pressure gauges at both the pump outlet and upstream of the load valve to account for test circuit pressure drop.
Verify all connections are rated for the maximum test pressure and that gauge snubbers are installed to protect instruments from pressure spikes during load valve manipulation.
Step 3 — Unloaded (No-Load) Flow Test
Start the pump and run at rated RPM with the load valve fully open (minimum resistance). Allow fluid temperature to stabilize within the specified test range, typically 45–55°C for mineral-based hydraulic oils.
Record the flow reading once stable. This unloaded value represents the pump's maximum volumetric output and should closely match the calculated theoretical flow from Step 1. A significant deficit at no-load indicates suction-side problems (inlet restriction, aeration) rather than internal pump wear.
Step 4 — Loaded (Full-Pressure) Flow Test
Gradually close the load valve to increase circuit pressure. Advance in increments of 25% rated pressure, recording flow at each step. This generates a flow-versus-pressure curve that reveals the pump's performance characteristics across its operating envelope.
At rated system pressure, record the stabilized flow value. This is the critical measurement for determining hydraulic pump efficiency under actual working conditions. The difference between no-load flow and full-pressure flow represents total internal leakage at operating pressure.
Never exceed the pump's rated maximum pressure during testing. Limit time at full pressure to what is necessary for a stable reading, typically 15–30 seconds for a standard test point.
Step 5 — Calculate Pump Efficiency
Volumetric Efficiency Formula
Volumetric Efficiency (%) = (Actual Flow at Rated Pressure ÷ Theoretical Flow) × 100
For example: a 45 cc/rev pump running at 1800 RPM has a theoretical flow of 81 LPM. If measured flow at rated pressure is 74.5 LPM, volumetric efficiency equals 91.9%.
Efficiency Interpretation Table
| Volumetric Efficiency | Pump Condition | Recommended Action |
|---|---|---|
| 95–100% | Excellent | Return to service; document baseline |
| 90–95% | Acceptable | Monitor at next scheduled interval |
| 85–90% | Marginal | Schedule rebuild or replacement |
| Below 80% | Failed | Remove from service immediately |
These thresholds serve as general guidelines. Some high-precision applications (servo systems, injection molding) may require tighter acceptance criteria, while less demanding circuits can tolerate slightly lower efficiencies before intervention becomes necessary.
Step 6 — Case Drain Flow Test (Internal Leakage Check)
For piston and vane pumps equipped with case drain lines, this test provides a direct measurement of internal leakage that bypasses the pumping elements and enters the housing.
Connect a low-range flow meter to the case drain port, routing flow back to the reservoir. Measure drain flow at both no-load and full system pressure. The difference quantifies pressure-dependent internal leakage, which directly correlates with wear on pistons, slippers, valve plates, or vane tips.
Compare measured case drain flow against the OEM maximum specification. Most piston pump manufacturers specify maximum acceptable case drain flow as a percentage of theoretical displacement, commonly 3–5% at rated conditions. Rising case drain flow tracked over time provides one of the clearest early indicators of hydraulic pump efficiency degradation.
Hydraulic Pump Pressure Testing Methods
While flow testing quantifies volumetric losses, pressure-specific diagnostics reveal control system behavior and help distinguish pump-related issues from circuit-level problems. Together, these methods enable complete hydraulic circuit troubleshooting.
Deadhead Pressure Test
This test verifies that the pump's maximum pressure output matches the system relief valve or compensator setting. Fully close the load valve and observe peak pressure on the gauge.
If pressure fails to reach the expected relief setting, the relief valve may be contaminated, worn, or improperly adjusted. If pressure overshoots, the relief valve may be stuck or the compensator is malfunctioning. Limit deadhead time to under 10 seconds for fixed displacement pumps to avoid excessive heat generation and potential shaft seal damage.
Pressure Ripple Analysis
High-frequency pressure transducers (sampling at 5–20 kHz) capture pressure pulsations that standard gauges cannot display. The frequency and amplitude of these ripples serve as diagnostic signatures for specific mechanical defects.
In gear pumps, tooth mesh frequency changes indicate gear wear or bearing degradation. In piston pumps, individual piston signatures reveal worn slippers, cracked pistons, or retaining plate issues. Analyzing these patterns requires baseline data from a known-good pump of the same model for comparison.
Load-Sense and Compensator Response Testing
Variable displacement pumps require additional validation of their control response. Test standby pressure with all circuit valves in neutral to confirm the pump de-strokes to minimum flow at the correct margin pressure setting (typically 200–400 PSI above load-sense signal).
Apply sudden load changes by rapidly cycling a directional valve and measure the compensator's response time. Sluggish response indicates contaminated control orifices, worn spool feedback mechanisms, or degraded control piston seals. These tests are essential for systems where dynamic response directly affects machine productivity.
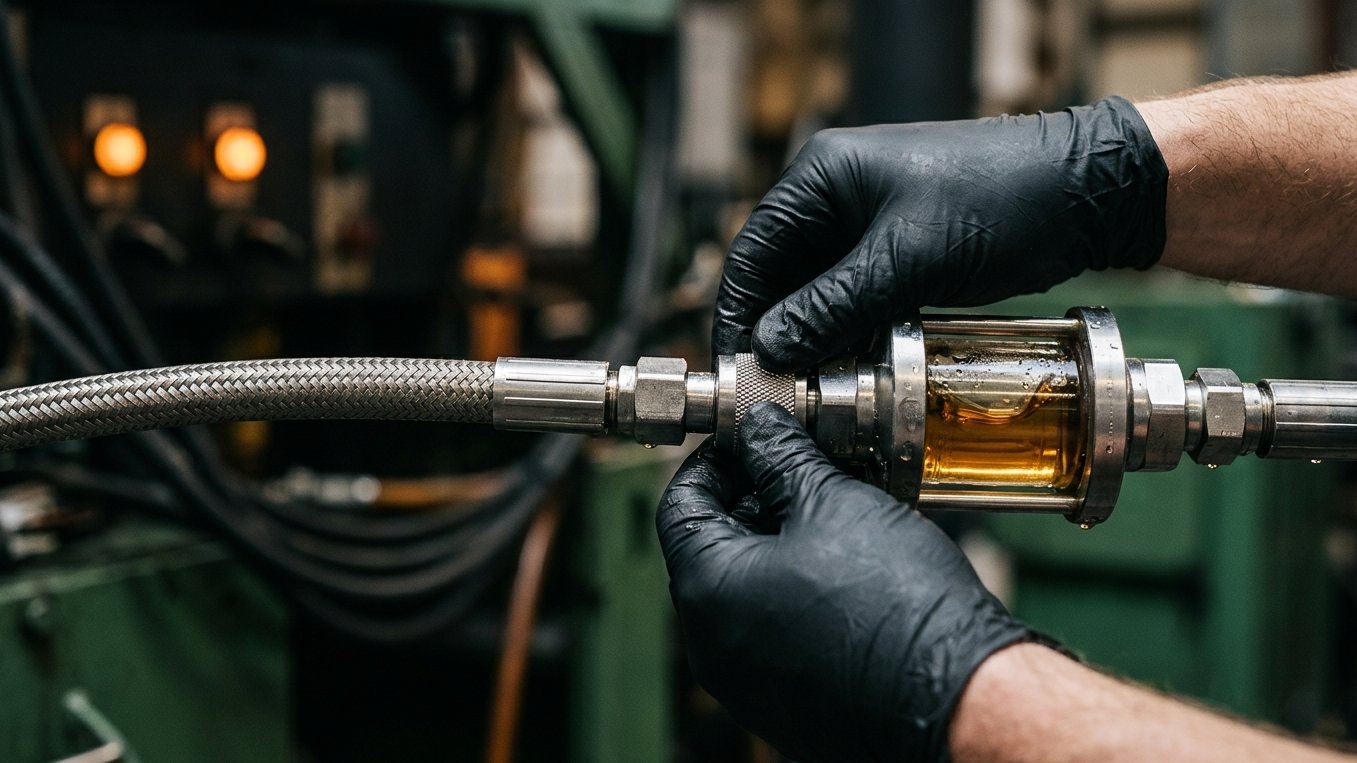
Interpreting Test Results and Identifying Failure Modes
Raw test data only becomes valuable when correlated with known failure patterns. The following guide helps translate measurements into targeted maintenance actions.
Correlating Flow Loss to Specific Wear Patterns
| Symptom | Likely Cause | Pump Type Most Affected |
|---|---|---|
| High case drain + low flow | Internal slipper/piston wear | Piston pumps |
| Flow drops only at high pressure | Worn vanes or cam ring | Vane pumps |
| Noisy operation + aerated flow | Inlet restriction or seal failure | All types |
| Erratic pressure at constant load | Worn valve plate or port plate | Piston pumps |
| Gradual efficiency decline over time | Normal wear progression | Gear pumps |
When to Rebuild vs. Replace
The rebuild-or-replace decision hinges on several factors beyond simple efficiency numbers. Consider the pump's criticality within the system, availability of rebuild kits, lead time for new units, and whether the failure mode suggests systemic contamination that could compromise rebuilt components.
As a general rule, if rebuild cost exceeds 60–65% of new pump price and the unit has already been rebuilt once, replacement provides better long-term value. Document all test results and repair decisions thoroughly to support warranty claims and establish lifecycle cost data for future purchasing decisions.
Advanced Diagnostic Techniques for Hydraulic System Diagnostics
Beyond standard bench and inline testing, modern maintenance programs leverage complementary technologies that extend visibility into pump health and system condition.
Thermal Imaging for Leak Detection
Infrared cameras reveal bypass leakage paths through differential temperature signatures. Internal leakage generates heat as pressurized fluid passes through tight clearances. Comparing thermal profiles across similar components under identical load conditions highlights units with abnormal internal bypass.
This technique is particularly effective for identifying failing check valves, internally bypassing relief valves, and worn motor drain cases without disconnecting any piping.
Oil Sampling and Particle Analysis
Wear metal analysis from fluid samples provides early warning of pump degradation months before efficiency losses become measurable with flow testing. Elevated copper and lead indicate bronze bearing or bushing wear. Iron particles suggest gear or housing erosion.
ISO 4406 cleanliness codes directly correlate with pump life expectancy. A pump rated for ISO 18/16/13 operating consistently at 21/19/16 may lose 50% or more of its projected service life. Particle counting validates filter performance and provides context for any efficiency test results.
Data-Logging and Trend Analysis
Continuous monitoring with pressure, temperature, and flow sensors recorded over operational cycles builds degradation curves specific to each pump installation. This data enables predictive maintenance scheduling based on actual wear rates rather than arbitrary time intervals.
Trend analysis reveals subtle changes invisible in periodic snapshot testing. A pump losing 0.5% volumetric efficiency per month may test as "acceptable" at any single point, but the trajectory clearly indicates a scheduled rebuild window 4–6 months ahead.
Testing Procedures by Pump Type
Gear Pumps
External gear pumps wear primarily at the gear tips, side plates, and housing bore. Testing focuses on comparing no-load to full-load flow since gear pumps have no case drain to measure. Efficiency losses are pressure-dependent and relatively linear.
Internal gear pumps (gerotor and crescent types) follow similar test procedures but typically exhibit tighter efficiency specifications when new and more rapid degradation once wear begins due to close-tolerance crescent or pin arrangements.
Vane Pumps
Vane pumps require attention to minimum operating speed during testing. Below a certain RPM threshold, vanes may not extend fully against the cam ring, producing artificially low flow readings unrelated to wear.
For cartridge-style vane pumps, compare test results against both new pump specifications and the specific cartridge kit specifications. Ring-and-vane kit replacement restores performance without full pump replacement if the housing and shaft remain within tolerance.
Piston Pumps (Axial and Radial)
Axial piston pumps offer the richest diagnostic data due to their case drain ports and multiple testable control parameters. Verify swashplate angle reaches full stroke by comparing maximum measured flow to theoretical displacement. Insufficient stroke suggests servo piston or control valve issues rather than pumping element wear.
Test barrel-to-valve plate condition by monitoring case drain flow response to pressure changes. A sharp, proportional increase in case drain with pressure confirms valve plate wear as the primary leakage path. Servo control response testing validates that displacement changes track command signals within manufacturer-specified time and accuracy bands.
Frequently Asked Questions
What is an acceptable volumetric efficiency for a hydraulic pump?
Most manufacturers consider 90% or above acceptable for continued operation in standard industrial applications. Below 85% typically warrants scheduling a rebuild or replacement. High-performance servo systems and injection molding circuits may require 93% or higher for adequate machine performance.
How often should hydraulic pumps be tested?
For critical systems where unplanned downtime carries significant cost, test every 500–1000 operating hours or quarterly, whichever comes first. Non-critical applications may extend intervals to semi-annually when supplemented by regular oil analysis monitoring between formal flow tests.
Can you test a hydraulic pump without removing it from the system?
Yes. Inline testing with a portable flow meter and load valve can be performed without pump removal in most circuit configurations. Install the test equipment between the pump outlet and the first directional valve. This approach is standard practice for hydraulic circuit troubleshooting in the field and saves significant labor compared to bench testing.
What causes a hydraulic pump to lose pressure but not flow?
This combination typically indicates a relief valve or compensator issue rather than pump wear. A worn pump loses flow under pressure but can still generate maximum pressure at reduced flow. Test the relief valve setting independently and inspect compensator control orifices before condemning the pump itself.
How does fluid temperature affect test accuracy?
Viscosity changes with temperature directly impact volumetric efficiency readings. Lower viscosity at elevated temperatures increases internal leakage, producing lower efficiency numbers. Always test at the OEM-recommended operating temperature range, typically 40–60°C (104–140°F), for valid comparisons against previous test records or manufacturer specifications.
What is the difference between volumetric and overall efficiency?
Volumetric efficiency measures flow losses from internal leakage, expressed as the ratio of actual output flow to theoretical flow. Overall (total) efficiency combines volumetric and mechanical efficiency, accounting for both leakage losses and friction or torque losses. Overall efficiency determines actual power consumption and heat generation, making it the more complete performance indicator for energy-focused maintenance programs.